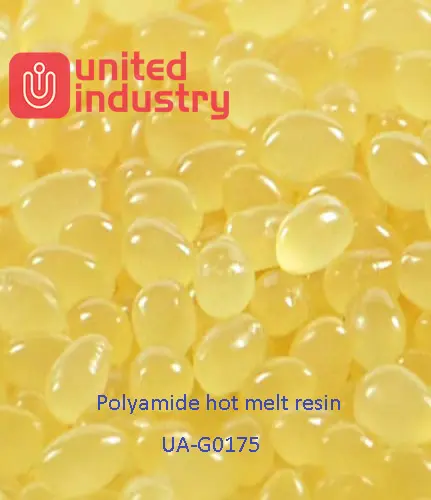
Polyamide Hot Melt Adhesive UA-G0175
UA-G0175 is a flame-retardant polyamide hot melt adhesive in amber granule form, developed for low pressure molding (LPM) of fragile and precision components in automotive electronics and filters, and for coating insulation. Its ring-and-ball softening point is 172–182 °C, it is processed between 190 and 230 °C, and it crystallises in 8 to 60 seconds — so an encapsulated part is cool, demoulded and packed while a potting resin would still be curing.
Low pressure molding is the reason this grade exists. Instead of overmoulding a connector, a sensor or a PCB area in engineering plastic at high temperature and high pressure, LPM injects molten adhesive into a closed mould at a fraction of that pressure: no damage to solder joints, wire insulation or MEMS, no chemical reaction during cure, no oven and no exotherm. Polyamide is the chemistry of choice because it pairs a high softening point with toughness and strong adhesion to the polar surfaces inside electronic assemblies — polyamide, PBT, FR-4, copper, brass and pretinned wire.
The property set is what separates UA-G0175 from a general-purpose hot melt. It carries a UL94 V0 flame rating, it is tested from −35 °C to +135 °C to the levels automotive and electronics programmes demand, and its dielectric behaviour at 10 GHz (Dk 3.3–3.7, Df 0.009–0.016) makes it usable around antenna, sensor and RF modules. Shore A 92 with elongation above 300% gives mechanical protection without the brittleness of a rigid potting compound, and because the seal is thermoplastic, a failed part can be reworked instead of scrapped.
Key Features
- UL94 V0 flame retardant — encapsulated assemblies meet a V0 requirement without a second flame-retardant process or added parts
- Tested from −35 °C to +135 °C — the temperature envelope automotive and electronics standards ask for, with a Tg of −35 °C
- Built for low pressure molding — a fraction of conventional injection pressure, so solder joints, wire insulation and MEMS survive encapsulation
- Crystallises in 8–60 seconds — cycle time in seconds, no curing oven and no post-bake; demould and pack
- Shore A 92 with ≥300% elongation — protects mechanically while absorbing thermal cycling and vibration instead of cracking
- RF-friendly dielectric — Dk 3.3–3.7 and Df 0.009–0.016 at 10 GHz suit antenna, sensor and high-frequency modules
- Reworkable — reheat the part and the encapsulant softens, so a failed component is repaired, not scrapped
- Amber granules in 20 kg kraft bags — dust-free and easy to meter into a hot melt tank
Technical Specifications
| Property | Value |
|---|---|
| Appearance | Amber granules |
| Softening point (ring and ball) | 172-182 °C |
| Melt viscosity | 3,500-5,500 mPa·s (210 °C) |
| Melt flow rate | 600-800 g/10 min (210 °C, 2.16 kg) |
| Hardness | Shore A 92 |
| Tensile strength | ≥6 MPa |
| Elongation at break | ≥300% |
| Glass transition temperature (Tg, DSC) | −35 °C |
| Service temperature, tested | −35 °C to +135 °C |
| Flammability | UL94 V0 |
| Dielectric constant Dk (10 GHz) | 3.3-3.7 |
| Dissipation factor Df (10 GHz) | 0.009-0.016 |
| Packaging | 20 kg kraft paper bags |
| Shelf life | 24 months (dry, room temperature, unopened) |
Processing Guidelines
| Stage | Guideline |
|---|---|
| Melting | 190-230 °C; keep within this window and avoid prolonged heating, which degrades the adhesive |
| Injection | Low pressure molding — a fraction of conventional injection pressure, set per mould, cavity and component fragility |
| Crystallisation and demoulding | 8-60 s per shot depending on part mass and wall section; no curing oven |
| Surface preparation | Remove dust and degrease the substrate with a suitable solvent before moulding |
| Moisture control | Polyamide absorbs water and damp granulate causes bubbles and weak bonds — dry at 80-100 °C for 2-4 hours before use if needed |
| Rework | Reheat the part to soften the encapsulant, repair, then remould |
Every mould and every assembly behaves differently. Send us the part drawing and we will advise on melt temperature, pressure and cycle before you commit to tooling.
Applications
- Automotive electronics — sensors, connectors, PCB areas and harness joints encapsulated by LPM where heat, vibration and a V0 flame requirement all apply
- Filters — end-cap bonding and pleat stabilization for air, oil and fuel filters, where the bond has to hold through heat, oil and vibration
- RF and sensor modules — antenna, radar and sensor assemblies that need a low-loss dielectric encapsulant
- Coating and insulation — protecting fragile components and conductive paths with a tough, void-free layer
- General assembly — anywhere a high-softening-point polyamide bond is needed on plastics, metals or pretinned surfaces
Why Choose Us
Shanghai United Industry Co., Ltd, founded in 2017, is a specialized manufacturer and exporter of hot melt adhesives — powders, films and polyamide grades — supplying customers worldwide. Every batch passes in-house checks on key parameters before shipment, so what you approve in sampling is what you receive in bulk production. We provide free technical consultation on melt temperature, injection pressure and cycle time, and support each customer from first sample through mass production. Packing is arranged to suit your line — 20 kg kraft bags, cartons or pallets — and makes us an easy partner for both trading companies and end users.
Frequently Asked Questions
What is low pressure molding, and why use a polyamide granule for it?
Low pressure molding injects molten hot melt into a closed mould at low pressure — a fraction of what conventional injection moulding needs — so fragile parts survive encapsulation. A polyamide granule is used because it combines a high softening point (172–182 °C here) with the toughness and adhesion electronic assemblies demand, and because granules melt cleanly in a hot melt tank without the dust of a powder.
Can UA-G0175 replace epoxy potting?
For many assemblies, yes, and with real process gains: 8–60 seconds instead of hours, no mixing, no curing oven, no exotherm, UL94 V0 without extra parts, and the part can be reworked rather than scrapped. Epoxy still wins where service temperature goes above the polyamide range or where resistance to aggressive solvents is essential. Tell us the service conditions and we will say honestly whether hot melt fits.
What temperature range does the encapsulated part survive?
UA-G0175 is tested from −35 °C to +135 °C, which covers the range automotive and electronics programmes typically specify, and its Tg is −35 °C so it stays flexible in cold service. Keep continuous service comfortably below the 172–182 °C softening point; above that the seal is thermoplastic and will soften.
Is it really flame retardant?
Yes — the grade carries a UL94 V0 rating, so a moulded part meets V0 without a second flame-retardant process. Confirm the rating with the wall section and geometry of your own part, as flame tests are thickness dependent.
Is it suitable for RF and antenna parts?
Yes. At 10 GHz the dielectric constant is 3.3–3.7 and the dissipation factor 0.009–0.016, which is low loss enough for antenna, radar and sensor modules. For critical RF designs we recommend measuring on your own stack-up.
The granules have absorbed moisture — what do I do?
Polyamide is hygroscopic, and damp granulate causes bubbles and weak bonds. Dry it at 80–100 °C for 2–4 hours before use, keep bags sealed between runs, and let cold bags come to room temperature before opening so condensation does not form inside.
What is the minimum order quantity, how is it packed, and can I get a sample?
There is no fixed MOQ — quantities are discussed according to your needs, and trial orders are welcome. Standard packing is 20 kg kraft paper bags, palletised for export, with 24 months shelf life in dry room-temperature storage. Samples are available so you can run them on your own melter and mould; email us your substrate, part drawing and annual volume.